
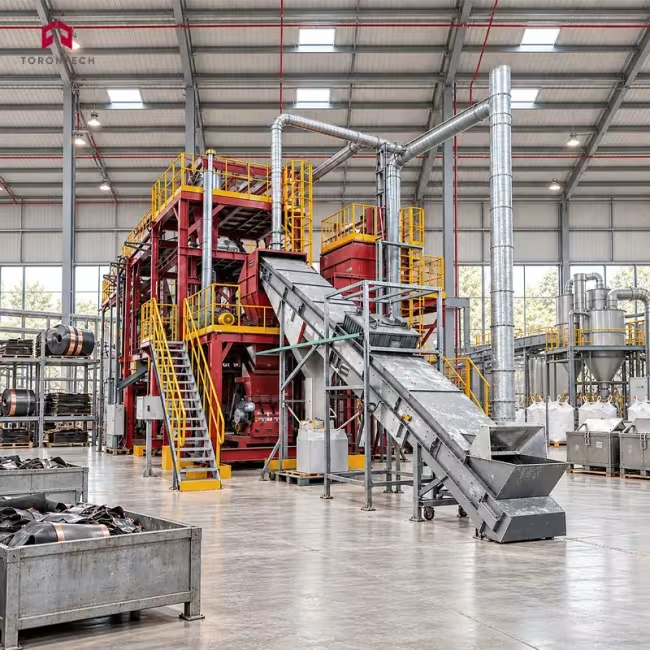
Lithium-Ion Electrode Scrap Recycling Line - ToronLi-ion™ ESR
ToronLi-ion™ ESR lithium-ion electrode scrap recycling line recovers coated cathode and anode sheets, stacking scrap, and laminate offcuts back into separated copper foil, aluminum foil, and electrode powder. Crushing, separation, and purification stages run as a fully automated sequence with limited manual handling. Recovery reaches more than 95 percent of reusable material according to supplier data. Cell manufacturers use the line to close the loop on internal production scrap rather than paying to dispose of coated foil.
Electrode scrap differs from whole-cell feedstock, and the process reflects that. Coating adheres to the current collector through a polymer binder, so the recovery problem is one of delamination rather than dismantling. The line strips that coating through staged mechanical working, supported by thermal treatment that breaks down binder and residual organic matter. Copper and aluminum foils granulate rather than pulverize, which creates the size and density contrast the sorting stages depend on.
Recovered electrode powder carries the valuable metal content of the original coating, including lithium, cobalt, and nickel, and it moves on to refiners for hydrometallurgical extraction. Copper granules and aluminum granules leave the line separated and ready for direct sale. A PLC governs the whole sequence, keeping operator involvement low and repeatability high across shifts. Automation also limits contact with fine powder, which matters for both product purity and workplace conditions.
Lithium-Ion Electrode Scrap Recycling Line - ToronLi-ion™ ESR Applications
The ToronLi-ion™ ESR line suits manufacturers generating coated electrode scrap and processors handling pole piece material as a dedicated stream.
- Battery Gigafactory Production Scrap: recovers coated foil rejected during coating, calendering, and slitting so material returns to the supply chain instead of going to disposal
- Electrode Coating Line Rejects: processes off-spec sheets from startup runs, coating defects, and changeover waste generated during normal production
- Cathode Sheet Recovery: separates aluminum current collector from cathode coating, recovering both the foil and the metal-bearing powder fraction
- Anode Sheet Recovery: parts copper foil from graphite coating, returning clean copper granules and recovered anode material
- Stacking and Laminating Scrap: handles laminate trim and stacking offcuts that carry coating on both faces
- Slitting and Calendering Offcuts: treats narrow edge trim and roll ends accumulated across converting operations
- Cathode Material Producers: closes an internal recovery loop so off-spec coated material returns to the powder supply
- Copper Foil Recovery: produces granulated copper stripped of coating for direct sale to metal buyers
- Aluminum Foil Recovery: converts coated aluminum current collector into clean granules through the same process route
- Black Powder Supply to Refiners: delivers screened electrode powder at consistent particle size for hydrometallurgical processing
- Pilot Line and R&D Scrap: processes small-volume development material where coating chemistry varies between batches
- Contract Electrode Manufacturers: adds recovery capability for scrap generated across multiple customer programs
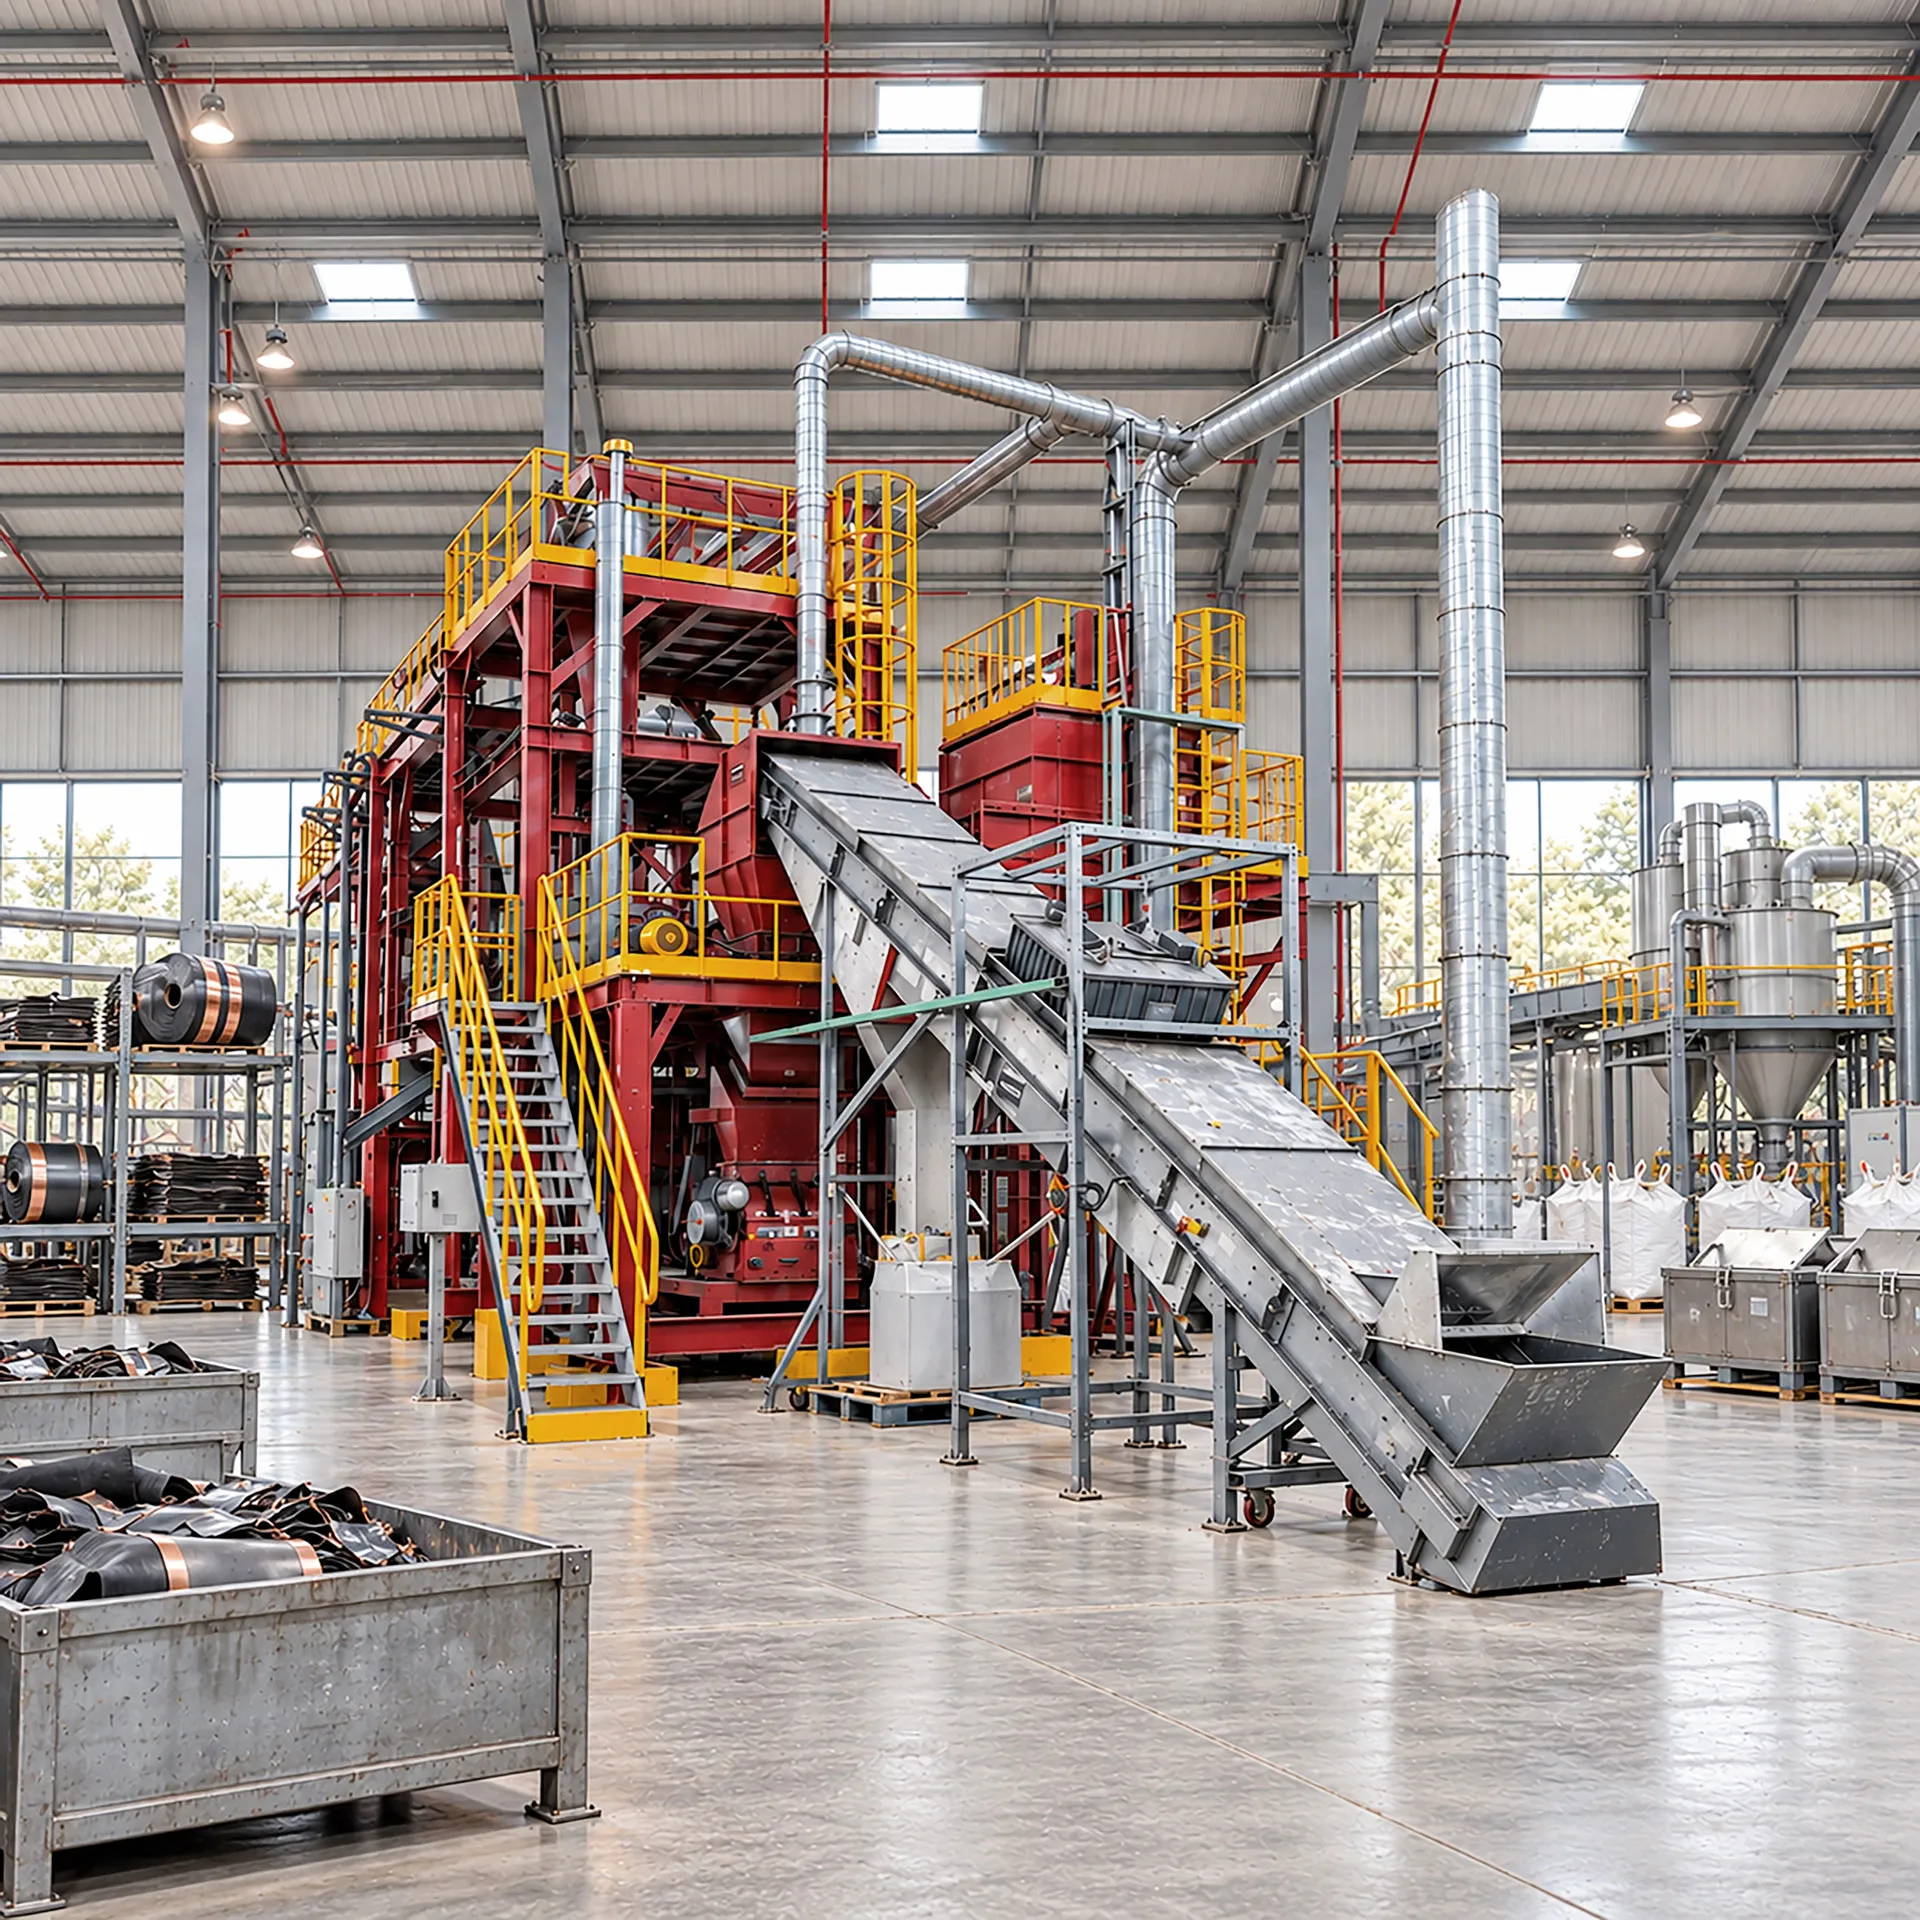
Lithium-Ion Electrode Scrap Recycling Line - ToronLi-ion™ ESR Key Features
The ToronLi-ion™ ESR line pairs staged crushing with thermal binder removal and three separate sorting principles, and each module can be specified against the electrode chemistry and scrap volume on site.
- Recovery Above 95 Percent: supplier data reports more than 95 percent of input returned as reusable material across the combined output streams
- Fully Automated Sequence: the process runs with limited manual intervention, which lowers labor cost and reduces operator contact with fine powder
- Precision Electrode Crushing: crushing action is tuned to coated sheet material rather than general scrap, protecting foil integrity while releasing coating
- Coating Stripping Fine Crusher: extended residence in the crushing cavity peels powder from the pole piece and converts copper and aluminum foil into granules
- Sealed Four-Shaft Crushing Chamber: the box body carries four-fold tightness and accepts nitrogen filling, holding down ignition risk when reactive material is present
- Low-Speed High-Torque Drive: slow shaft rotation with high torque cuts coated sheet quietly and without the heat buildup faster cutters generate
- Automatic Reverse and Overload Protection: PLC-managed start, stop, reverse, and overload response clears jams without opening the cutting chamber
- Controlled Drying Stage: operation between 100 and 150 degrees Celsius removes organic matter while leaving film material undamaged for later sorting
- Low-Temperature Cracking Furnace: operation between 450 and 600 degrees Celsius decomposes binder and residual organics, raising recovered powder quality
- Three-Stage Exhaust Treatment: catalytic combustion, alkali washing and spraying, and activated carbon polishing bring the gas stream to emission requirements
- Static and Dynamic Screening Combined: linear screens, circular vibrating screens, and airflow sorting screens work together to draw powder out thoroughly
- Air Sorting at 99 Percent: airflow classification separates light material from heavy material at a supplier-reported ratio of 99 percent
- Gravity Sorting at 99 Percent: specific gravity sieving parts copper granules from aluminum granules at a supplier-reported ratio of 99 percent
- Siemens PLC Central Control: one program governs the process, with Ethernet, MODBUS TCP/IP, OPC, PROFINET, and DP interfaces reserved for DCS integration
- Branded Electrical Components: control cabinets are built with ABB, Schneider, and Siemens components for parts availability and service familiarity
- Reduced Environmental Load: recovering coated foil keeps battery manufacturing waste out of disposal streams and returns metal content to production
Theory and Method
Electrode recovery is a delamination problem. Coating sits on the current collector as a particulate layer held in place by a polymer binder, typically polyvinylidene fluoride on the cathode side. That bond resists simple crushing because the foil beneath it deforms rather than fractures. The line works around this by combining mechanical action with thermal treatment: heating decomposes the binder and releases its grip, while repeated crushing shears the loosened coating away from the metal surface.
Foil behavior then does the sorting work. Copper and aluminum are ductile, so crushing tears them into curled granules rather than reducing them to powder. Coating, by contrast, is brittle and breaks down into fines. Two populations emerge with a wide particle size gap between them, and screening separates the powder fraction from the granules on that basis alone. Extended residence in the fine crusher cavity carries this further, stripping remaining coating while the granules take their final form.
Metal separation relies on density. Copper sits near 8.96 grams per cubic centimeter against aluminum near 2.70, a difference large enough for gravity methods to exploit reliably. Specific gravity sieving fluidizes the granule bed so denser copper migrates downward and stratifies away from aluminum, with a supplier-reported sorting ratio of 99 percent. Air classification handles the lighter end of the stream, separating film and low-density residue at a reported separation ratio of 99 percent.
Lithium-Ion Electrode Scrap Recycling Line - ToronLi-ion™ ESR Technical Specifications
System Overview
| Parameter | Specification |
|---|---|
| System Type | Automated crushing, thermal treatment, and sorting line for lithium battery electrode scrap |
| Processable Feedstock | Cathode and anode electrode plates, pole pieces, stacking and laminate scrap, coated foil offcuts |
| Output Materials | Electrode powder, copper granules, aluminum granules, separated film material |
| Recovered Metal Content | Electrode powder carrying lithium, cobalt, and nickel for downstream refining |
| Material Recovery Rate | Over 95 percent of reusable material (supplier stated) |
| Crushing Chamber Sealing | Four-fold tightness, suitable for nitrogen filling |
| Drying Temperature | 100 to 150 °C |
| Cracking Furnace Temperature | 450 to 600 °C |
| Air Sorting Ratio | 99 percent (supplier stated) |
| Gravity Sorting Ratio | 99 percent (supplier stated) |
| Control System | Siemens PLC with central control cabinet |
| Communication Interfaces | Ethernet with independent IP address, MODBUS TCP/IP, OPC, PROFINET, DP |
| Electrical Components | ABB, Schneider, Siemens |
| Automation Level | Fully automated process with minimal manual intervention |
| Layout | Modular, floor space customized to the site |
Machine Line-Up
The line is assembled from the modules below. Each stage is described with its function, working method, and available parameters.
1. Feeding System
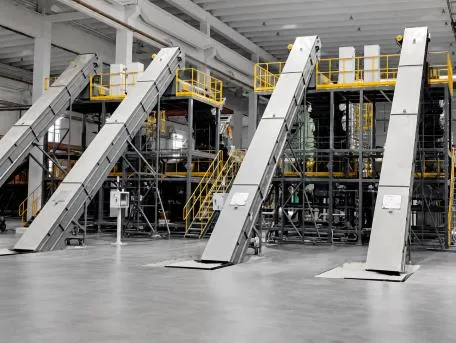 | Electrode scrap is charged onto the infeed conveyor and metered into the crushing stage at a controlled rate. Steady feeding keeps the crusher inside its torque band and prevents surge loading from dense bundles of stacked sheet. |
| Parameter | Specification |
|---|---|
| Function | Meters electrode scrap into the crushing system at a controlled rate |
| Feed Material | Loose sheet, stacked laminate, roll ends, and trim |
| Discharge | Direct into crushing chamber |
| Configuration | Sized to line throughput and scrap format |
2. Crushing System
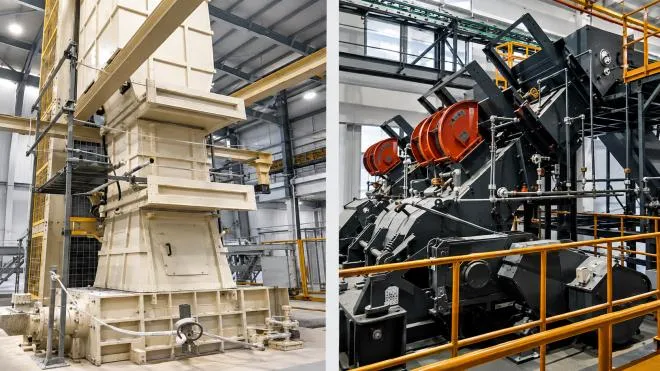 | The coarse crusher is a four-shaft shredder built for lithium battery duty. The box body carries four-fold sealing so the chamber can be filled with nitrogen, which lowers oxygen around the cutting zone and holds down the risk of ignition when charged cells are cut. Cells and modules reduce rapidly into flake material. Microcomputer control manages start, stop, reverse, and overload response automatically, and the drive runs at low speed with high torque and low noise. |
| Parameter | Specification |
|---|---|
| Function | Primary size reduction of electrode plates and laminate into flake material |
| Rotor Configuration | Four-shaft shredder |
| Chamber Sealing | Four-fold tightness, suitable for nitrogen filling |
| Atmosphere Control | Gas protection design available |
| Safety Provision | Multi-level protection measures against fire risk |
| Drive Characteristics | Low speed, high torque, low noise |
| Control Functions | Automatic start, stop, reverse, and overload reverse |
| Electrical Control | Designed to align with European CE requirements (certificate number not supplied) |
| Output Form | Flake material for downstream treatment |
3. Drying System
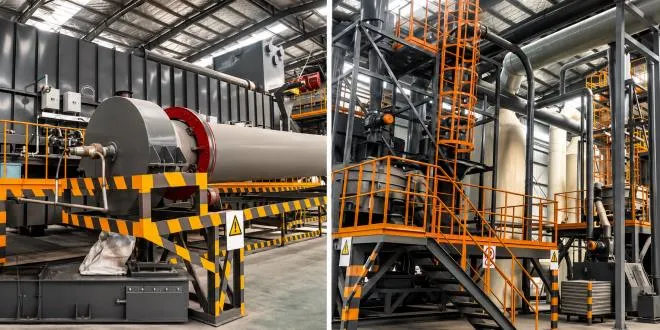 | Crushed material passes through a drying stage held between 100 and 150 degrees Celsius. Organic matter volatilizes at this temperature and is condensed for recovery. The range sits below the point at which film material breaks down, so that fraction stays intact and remains sortable further along the line. |
| Parameter | Specification |
|---|---|
| Function | Volatilization and recovery of organic matter from crushed material |
| Operating Temperature | 100 to 150 °C |
| Recovery Method | Condensation of volatilized organics |
| Film Condition | Film material remains undamaged at this temperature |
| Process Purpose | Prepares material for sorting and reduces load on the exhaust system |
4. Cracking and Pyrolysis System
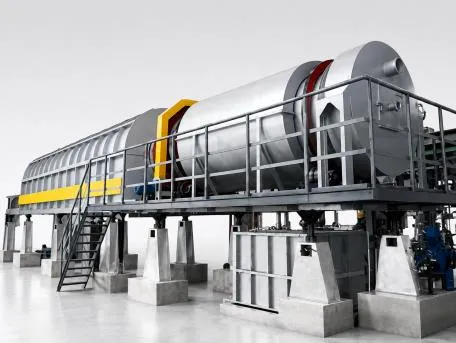 | The cracking furnace runs a low-temperature pyrolysis process between 450 and 600 degrees Celsius. Organic matter and impurities remaining in the crushed battery material decompose at this temperature, including the polymer binder that holds coating to the current collector foil. Removing that binder raises the purity of the black powder recovered downstream. |
| Parameter | Specification |
|---|---|
| Function | Thermal decomposition of binder, organic matter, and residual impurities |
| Furnace Temperature | 450 to 600 °C |
| Process Type | Low-temperature cracking |
| Target Material | Polymer binder and organic impurities in crushed electrode material |
| Process Benefit | Raises the quality of recovered electrode powder |
5. Exhaust Gas Treatment System
Gas from drying and cracking passes through a three-stage treatment train. Catalytic combustion destroys combustible organic content, alkali washing and spraying neutralizes acidic and harmful components, and activated carbon polishes the remaining stream before discharge.
| Parameter | Specification |
|---|---|
| Function | Removal of harmful substances from process exhaust gas |
| Stage 1 | Catalytic combustion |
| Stage 2 | Alkali washing and spraying |
| Stage 3 | Activated carbon purification |
| Discharge Condition | Treated to meet applicable emission requirements |
6. Secondary Crusher
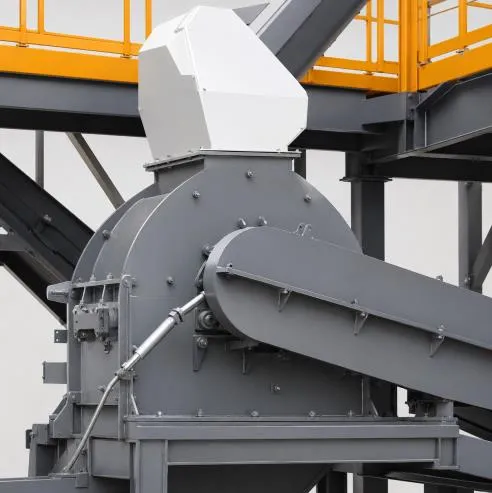 | A high-speed single-shaft hammer crusher handles intermediate size reduction. The hammer action breaks up bulk material remaining after thermal treatment, which prepares the stream for separation of heavy components such as steel shells and pole lugs by specific gravity. |
| Parameter | Specification |
|---|---|
| Function | Intermediate size reduction after thermal treatment |
| Crusher Type | High-speed single-shaft hammer crusher |
| Target Material | Bulk material remaining in the process stream |
| Process Purpose | Prepares heavy fractions for gravity sorting |
7. Fine Crusher
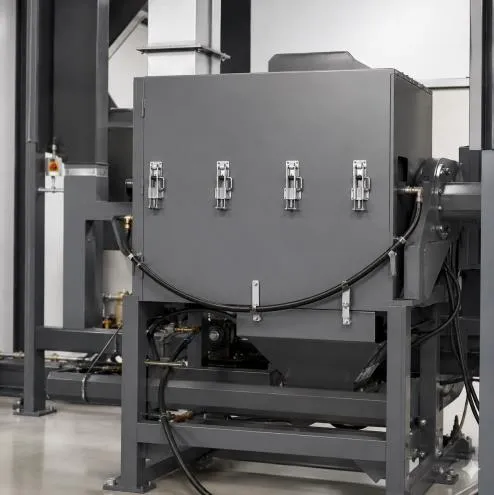 | The fine crusher completes the liberation of coating from foil. Material is held in the crushing cavity for an extended period rather than passing straight through, and repeated working peels black powder off the pole piece while turning copper foil and aluminum foil into granules. Granulating the foils is what allows copper and aluminum to be parted cleanly at the sorting stage. |
| Parameter | Specification |
|---|---|
| Function | Stripping of coating from electrode foil and granulation of current collectors |
| Residence Behavior | Extended retention in the crushing cavity |
| Output Form | Copper granules, aluminum granules, liberated electrode powder |
| Process Purpose | Enables clean copper and aluminum separation downstream |
8. Screening System
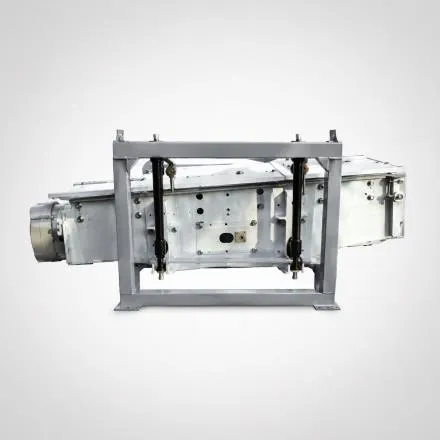 | Screening runs across several machine types selected by process route. Linear screens, circular vibrating screens, swing screens, and airflow sorting screens combine static and dynamic action so black powder is drawn out of the material thoroughly rather than in a single pass. |
| Parameter | Specification |
|---|---|
| Function | Separation of electrode powder from granule and coarse fractions |
| Screen Types | Linear screen, circular vibrating screen, airflow sorting screen |
| Screening Method | Combined static and dynamic screening |
| Selection Basis | Screen type chosen according to the process route |
| Process Benefit | Raises the recovery rate of electrode powder |
9. Air Sorting System
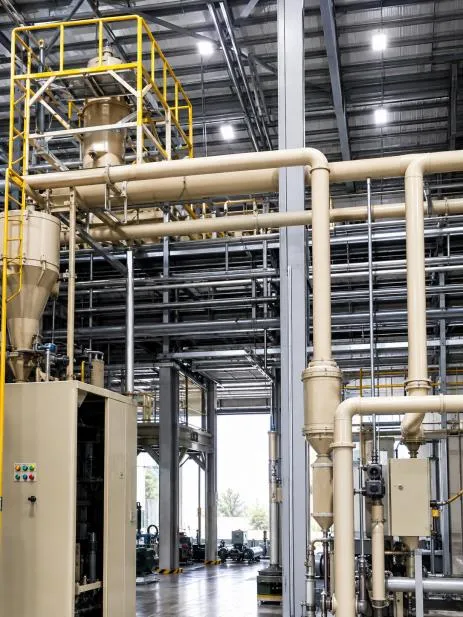 | The air sorting system directs a controlled airstream through the material. Light material travels with the flow while heavy material resists it and falls, which splits film and low-density residue from metal granules. |
| Parameter | Specification |
|---|---|
| Function | Separation of light material from heavy material |
| Working Principle | Airflow direction and terminal velocity difference |
| Separation Ratio | 99 percent (supplier stated) |
| Light Fraction | Film material and low-density residue |
| Heavy Fraction | Copper and aluminum granules |
10. Gravity Sorting System
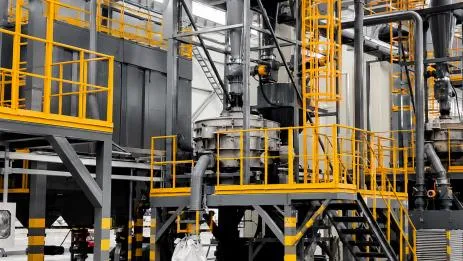 | Gravity sorting completes the metal separation. Residual black powder is first sieved out of the copper and aluminum granules, and a specific gravity sieving machine then parts the two metals using the density difference between them. |
| Parameter | Specification |
|---|---|
| Function | Separation of copper granules from aluminum granules |
| Working Principle | Specific gravity difference under sieving action |
| Preliminary Step | Sieving of residual black powder from the granule stream |
| Sorting Ratio | 99 percent (supplier stated) |
| Output Fractions | Copper granules, aluminum granules, recovered black powder |
11. Central Control System
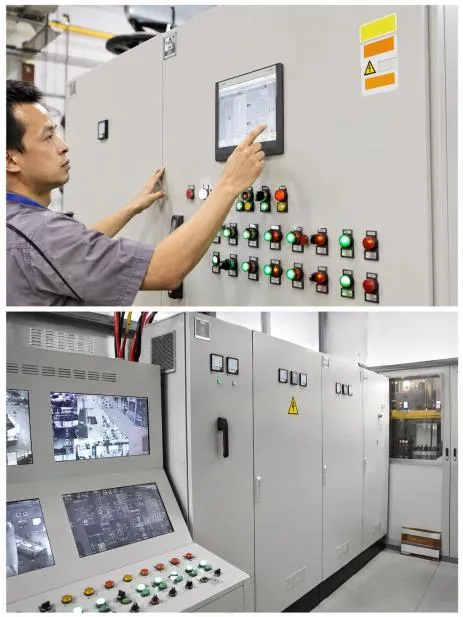 | Electrical design across the whole process runs under a Siemens PLC program. The controller reserves an Ethernet port with an independent IP address supporting MODBUS TCP/IP, OPC, and PROFINET, plus a DP communication interface, so the line integrates with a plant DCS and supplies the corresponding variable table. Control cabinets are built with ABB, Schneider, and Siemens components. |
| Parameter | Specification |
|---|---|
| Function | Process sequence control, monitoring, and plant integration |
| Controller | Siemens PLC |
| Network Interface | Ethernet port with independent IP address |
| Supported Protocols | MODBUS TCP/IP, OPC, PROFINET, DP |
| Plant Integration | DCS communication with variable table provided |
| Component Brands | ABB, Schneider, Siemens |
| Cable Management | Cable trays laid according to site requirements |
| Operation | Centralized automatic control across all modules |